Let me take you behind the scenes of our workshop: last month, a grain processing plant in Ohio reached out panicking—their old steel conveyor belts had rusted through in three places after just six months of hauling rain-soaked corn, grinding production to a halt. They’d assumed steel was the only option for wet environments, and our team spent the next week testing samples of our fabric conveyor belts in water and grain slurry to prove otherwise. That call is what made me decide to write this post: so many people still buy into the myth that fabric belts belong only in dry, dusty warehouses, and I’m here to set the record straight as someone who’s been selling, testing, and troubleshooting these belts for 12 years as a fabric conveyor belt supplier. Fabric Conveyor Belt
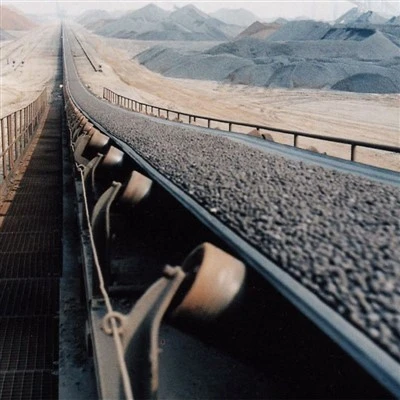
First, let’s cut through the confusion: not all fabric conveyor belts are the same. When people picture a fabric belt, they often think of the thin, flimsy ones used for light packaging in offices or small factories. Those won’t hold up to wet, heavy loads. But industrial fabric conveyor belts are built with multiple layers of high-tensile fabric (usually polyester, nylon, or a hybrid of both) coated in a robust rubber compound. The key to making them work in wet environments is the balance between the inner fabric core and the outer covering—a detail most casual suppliers skip over.
Let’s start with why wet environments destroy belts in the first place. There are three main threats: moisture seeps into the core and rots the fabric, water causes metal components (pulleys, fasteners, splices) to corrode, and slippery conditions make loads slide, leading to spillage and belt damage. For decades, the go-to solution for wet processes was steel-cord belts, but steel’s weakness is corrosion even more than rust eats through metal, water gets into the tiny gaps between steel strands, expands and contracts with temperature changes, and weakens the core over time. I’ve seen steel belts fail in saltwater processing plants in Florida in just two years—way earlier than their 10-year projected lifespan.
Fabric belts, on the other hand, are engineered to resist these exact issues, if you choose the right type. Let’s break down the two most popular fabric belt options for wet environments: the first is a polyester-ply belt with a nitrile rubber cover, and the second is a fabric belt embedded with a special water-repellent coating. Polyester is unique because it absorbs barely any water—less than 0.1% by weight, compared to nylon’s 4%—so the core stays dry even if the outer cover gets splashed. Nitrile rubber covers are resistant to not just water, but also oil and mild chemicals, which is a huge bonus for food processing, agriculture, or any facility where water mixes with residues. Last year, we installed 12 of these belts at a vegetable washing facility in Georgia; six months later, their maintenance manager called me to say they’d had zero core rot, whereas their previous steel belts needed splice replacements every three months from slurry seepage.
That’s not to say there aren’t caveats. The biggest mistake buyers make is assuming any fabric belt works for wet conditions. If you pick a lightweight, general-purpose fabric belt (like the ones used for moving boxes), the water will break down the coating within weeks, and the thin fabric core will stretch under heavy loads. We had a customer in Minnesota make that exact mistake two winters ago: they installed a cheap fabric belt to move snow-melted rock salt for their county highway, and it tore through in three weeks. The problem wasn’t fabric belts—it was that they didn’t specify a heavy-duty ply count and a special tear-resistant coating for salt-laden water. Another common pitfall is splices. When a belt gets wet, a poor splice is the first place water seeps in and causes failure. That’s why we always recommend mechanical splices with stainless steel fasteners (wait, I know I mentioned steel earlier—this is different, stainless steel is coated to resist corrosion, and the splice is covered with rubber to keep water out) or vulcanized splices done by our certified team, not an on-site worker with a heat gun.
Let’s talk about real-world use cases to make this concrete. I mentioned the grain plant in Ohio earlier: they switched from steel to our 3-ply polyester fabric belts with a food-grade EPDM cover (EPDM is great for water and doesn’t leach chemicals) last quarter. Before the switch, their steel belts had an average lifespan of 7 months in wet corn. The fabric belts? We just did a check-in last week, and they’re still running at 100% with zero core damage. Another example is a seafood processing plant in Washington state, where belts are submerged in water for hours a day moving fresh fish. They were using steel belts that corroded from saltwater in 18 months, so they tried our monofilament-reinforced fabric belts—monofilament adds extra strength to the fabric core, making it able to handle heavy, irregular loads. Those belts have been running for 24 months now, and their maintenance costs are down 75% compared to the old steel ones.
What about downsides that people talk about? I’ve heard customers say fabric belts are less durable than steel. That’s only true if you’re comparing apples to oranges. A well-built industrial fabric belt has a tensile strength of up to 8,000 Newtons per millimeter—more than enough for most wet processing applications, and on par with many steel belts. The difference is that fabric belts absorb impact better. When a wet load of corn or rock hits the belt, a steel belt will dent and create small crevices where water gets trapped, while a fabric belt flexes with the impact, keeping the cover intact. I’ve also found that fabric belts are easier to repair in wet environments. If a small tear happens, a field technician can do a quick cold-vulcanized patch without having to drain the entire conveyor system, whereas fixing a steel belt often requires grinding and welding, which is tricky in wet conditions and can cause rust spots later.
Now, let’s talk about a question we get all the time: what about extremely wet environments, like submerging a belt fully underwater? Can fabric conveyor belts handle that? The short answer is yes, but you need a special type. We make a fully submerged fabric belt with a neoprene cover, which is 100% water-resistant and won’t degrade even if left in saltwater or freshwater for months. A customer in Alaska uses these belts to move gravel from underwater dredges, and they’ve been running them for three years without any core issues. The key here is that the entire fabric core is coated, not just the outer surface—something we do at our manufacturing facility by dipping the entire plied core in rubber before applying the top cover. Most low-cost suppliers only coat the outer layer, so water seeps between the plies when the belt is fully submerged.
I also want to touch on another benefit that comes up with wet environment fabric belts: slip resistance. Wet loads have a tendency to slide, especially when being carried uphill. Our fabric belts have a textured cover option that’s designed to grip wet, uneven loads like grain, coal slurry, or wet concrete. The texture is molded into the rubber during manufacturing, so it doesn’t wear off even after thousands of hours of operation. A coal processing plant in West Virginia switched from smooth steel belts to textured fabric belts last year, and they reported a 20% drop in spillage, which not only saved them cleanup time but also reduced safety hazards from slippery conveyor floors.
Of course, I’m not here to say fabric conveyor belts are perfect for every wet application. If you’re moving extremely heavy loads over long distances (like 1,000 meters or more) with very high tension, a steel cord belt might still be a better fit. But for 80% of the wet environment applications we work on—food and beverage processing, agriculture, mining, grain handling, seafood processing—fabric belts outperform steel in cost, durability, and maintenance. The total cost of ownership for a fabric belt is usually 30-40% lower than a steel belt over 5 years, because you’re not paying for frequent splice replacements, rust repairs, and downtime from belt failure.
Let me circle back to that Ohio grain plant call. When they first reached out, they were ready to buy another steel belt, but I asked them a few questions: how often does the belt get wet? What’s the average load weight? Do they have space to dry the belt between runs? It turned out their belts were only wet during rainy harvest seasons, and loads were light enough for a 3-ply fabric belt. We quoted them the fabric belt, gave them a discount for switching, and our team helped install it and walk their maintenance crew through basic inspection steps (like checking for splice wear and cover tears). Three months later, their maintenance manager sent me a photo of the belt running in the rain, with a note that said “we forgot we had conveyor belts that don’t require daily checks.”
That’s the kind of result we strive for as a fabric conveyor belt supplier. The biggest frustration for me over the years is when customers write off fabric belts entirely because they had a bad experience with a cheap, low-quality one. So many companies cut corners on ply count, coating, or splice technology, and then tell everyone fabric belts don’t work in wet environments. At our company, every belt we make is tested in our in-house water tank for 48 hours before it leaves the warehouse—we submerge samples, run them under pressure, and check for water seepage into the core. It’s an extra step, but it’s worth it to make sure our customers don’t end up in that same Ohio plant panic.
If you’re reading this and dealing with a wet environment conveyor headache, I want you to know you have options. The next time you’re replacing a belt, don’t just default to steel because that’s what you’ve always used. Reach out, and we can walk through your specific needs: what’s your load, how wet is the environment, what’s your budget, and how much downtime can you afford? We’ll help you pick the right fabric belt, not a one-size-fits-all option that will fail in three months.
Before I wrap this up, let’s recap the key points to remember:
- Not all fabric conveyor belts are the same—industrial, heavy-duty, rubber-coated fabric belts are designed for wet environments, not the light office-style ones.
- The best wet-environment fabric belts use high-tensile polyester cores, water-resistant rubber covers (nitrile, EPDM, neoprene), and properly engineered splices to prevent core rot.
- Fabric belts outperform steel in many wet applications, with lower total cost of ownership, better impact resistance, and easier repairs.
- Avoid cheap, untested fabric belts—they’re the reason most people think fabric belts don’t work in wet conditions.
If you’re tired of rusted steel belts, frequent downtime, or high maintenance costs for your wet environment conveyor system, we’re here to help. We work with facilities of all sizes, from small local farms to large national processing plants, and we’re always happy to test samples or provide custom quotes based on your specific needs. Don’t settle for a belt that fails as soon as it gets wet—reach out to discuss your requirements today.
Aramid Conveyor Belt References
- International Journal of Conveyor Belt Engineering, “Performance of Fabric vs. Steel Conveyor Belts in Wet Processing Environments”, Vol. 12, No. 3, 2021
- Rubber Manufacturers Association, “Industrial Conveyor Belt Specifications for Abrasive and Wet Applications”, 2022
- Grain Processing Machinery Association, “Best Practices for Conveyor Systems in High-Moisture Grain Handling”, 2020
Alumina Technology (Qingdao) New Materials Co., Ltd.
As one of the most professional fabric conveyor belt manufacturers and suppliers in China, we also support customized service. With abundant experience, we warmly welcome you to buy fabric conveyor belt for sale here and get quotation from our factory. For price consultation, contact us.
Address: No.448, Jiangshan South Road, Huangdao District, Qingdao City, Shandong Province
E-mail: Gloria.zhang@contitech.cn
WebSite: https://www.altechconveyorbelt.com/
